Line and application survey
Review products, defects, speed, access, environment, controls and the action required after a fail.
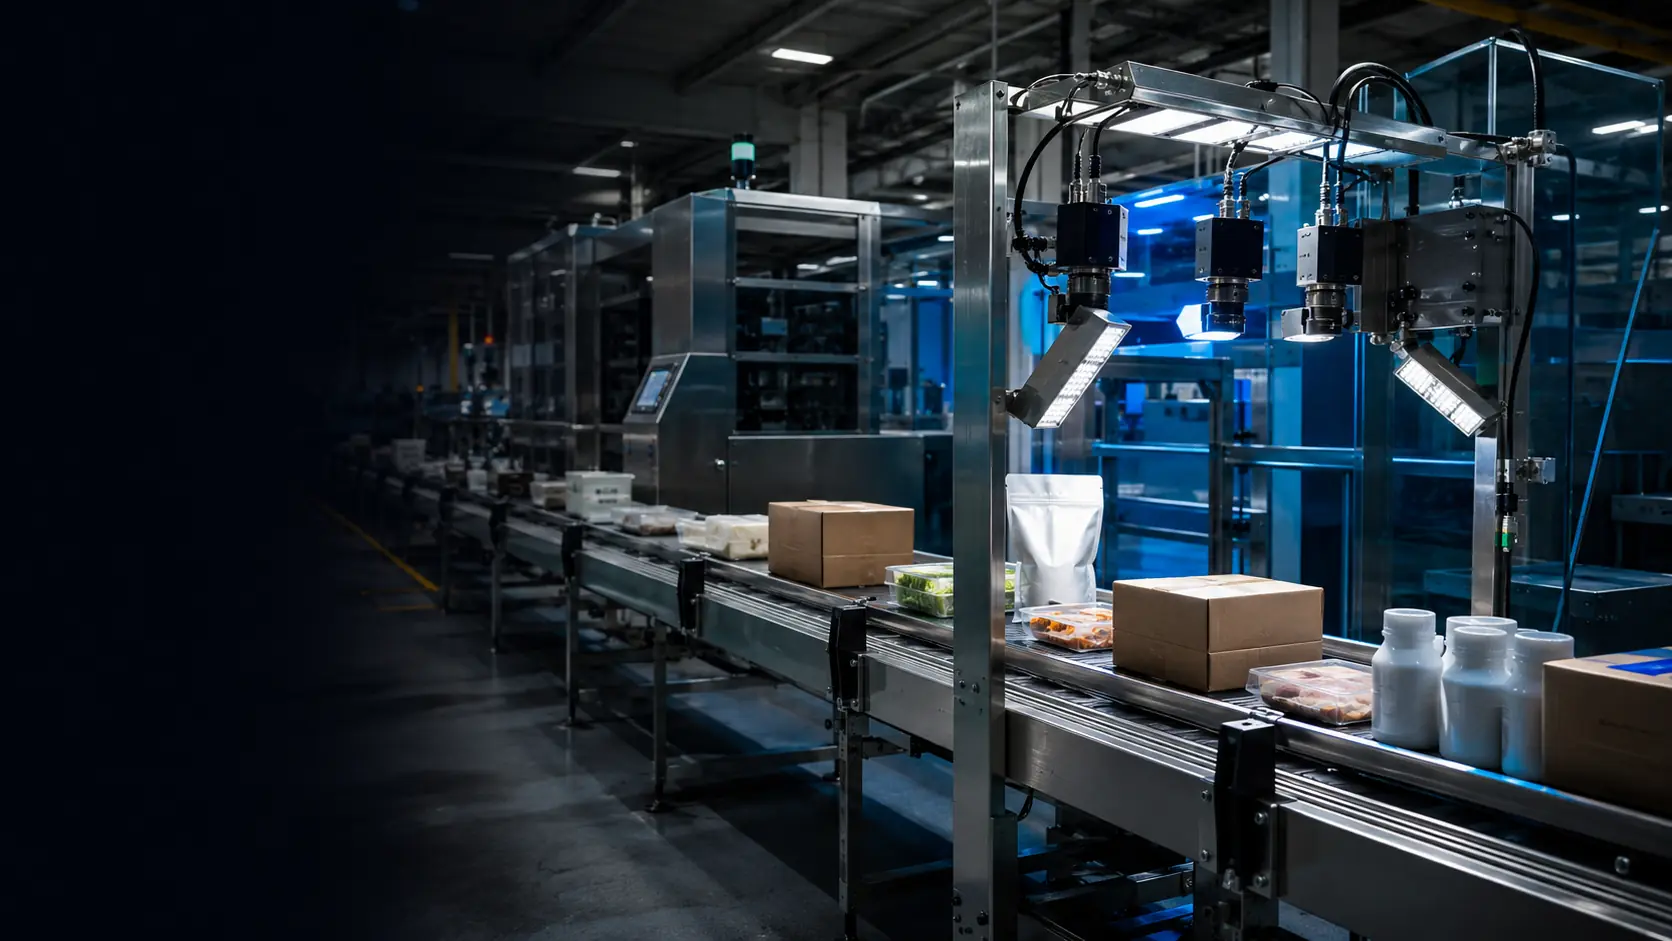
Add automated camera inspection to an existing line with the mechanics, controls, tracking and reject response engineered as one working system.
 Application-led imaging Proved with the real product, defect and line conditions.
Often, yes. A successful retrofit starts with a line survey covering product presentation, camera access, controlled lighting, PLC signals, guarding, available reject space and changeovers. The inspection method is then proved before the final mechanical and controls design is fixed.
Every check is confirmed against the real product, defect set, line speed and production environment before final specification.
Review products, defects, speed, access, environment, controls and the action required after a fail.
Use representative good and failed samples to prove camera, lens, lighting and inspection logic.
Design mounts, enclosures, lighting, guarding and access around operators, cleaning and maintenance.
Define triggers, recipes, handshakes, alarms, bypass control, fault states and production data.
Track the inspected product to a reject, divert, stop or alarm point and confirm the response.
Test against agreed samples and criteria, document settings and train production users.
Available line space, field of view, product spacing and stability, speed, controls compatibility, reject distance, safe access, cleaning requirements, product recipes and the exact defect set.
Oxford Vision Systems can take responsibility for the inspection chain from image formation to line response. That includes the camera hardware, inspection software, mechanical design, electrical integration, operator interface, data requirements and acceptance test.
Not every line can accept a dependable retrofit without changes. Crowded layouts, uncontrolled product movement or no reject space may require conveyor modifications or relocation of the inspection point. The survey makes those constraints visible before investment.
Use these related pages to compare the inspection methods and production environments that may form part of the project.
Provide line photos or video, product range, target defects, line speed, product spacing, available reject point, controls information and representative samples where possible.
Yes, subject to survey. We review the existing optics, mounts, controls, recipes, signals and inspection requirement before proposing a replacement architecture.
Yes, where the line can accommodate a suitable reject or divert method and the product can be tracked reliably from camera to reject point.
We test representative good products, known defects and normal variation under a controlled optical arrangement, then agree measurable acceptance criteria before final build.
Identify the inspection task and the available point on the line, including product presentation and space for cameras and lighting. Define the signal interfaces and any reject requirement. Assess representative samples under the proposed conditions, then agree how product changes and inspection failures will be managed.
Related guidance: System cost guide · Specification guide
Send us samples, images, line-speed information and the defects you need to detect. We’ll recommend the right next step.