Scratches, dents, chips and edge damage
Configured against agreed examples, limits and the required line response.
Surface inspection looks for visible departures from an accepted appearance. The challenge is making the target defect stand out while allowing harmless texture and finish variation.
We select bright-field, dark-field, diffuse, backlight or structured illumination according to how the defect interacts with light, then prove the inspection on good and bad samples.
We start with representative products, known defects, acceptable variation, line speed and the required response. That evidence determines the field of view, resolution, optics, processing and mechanical design.
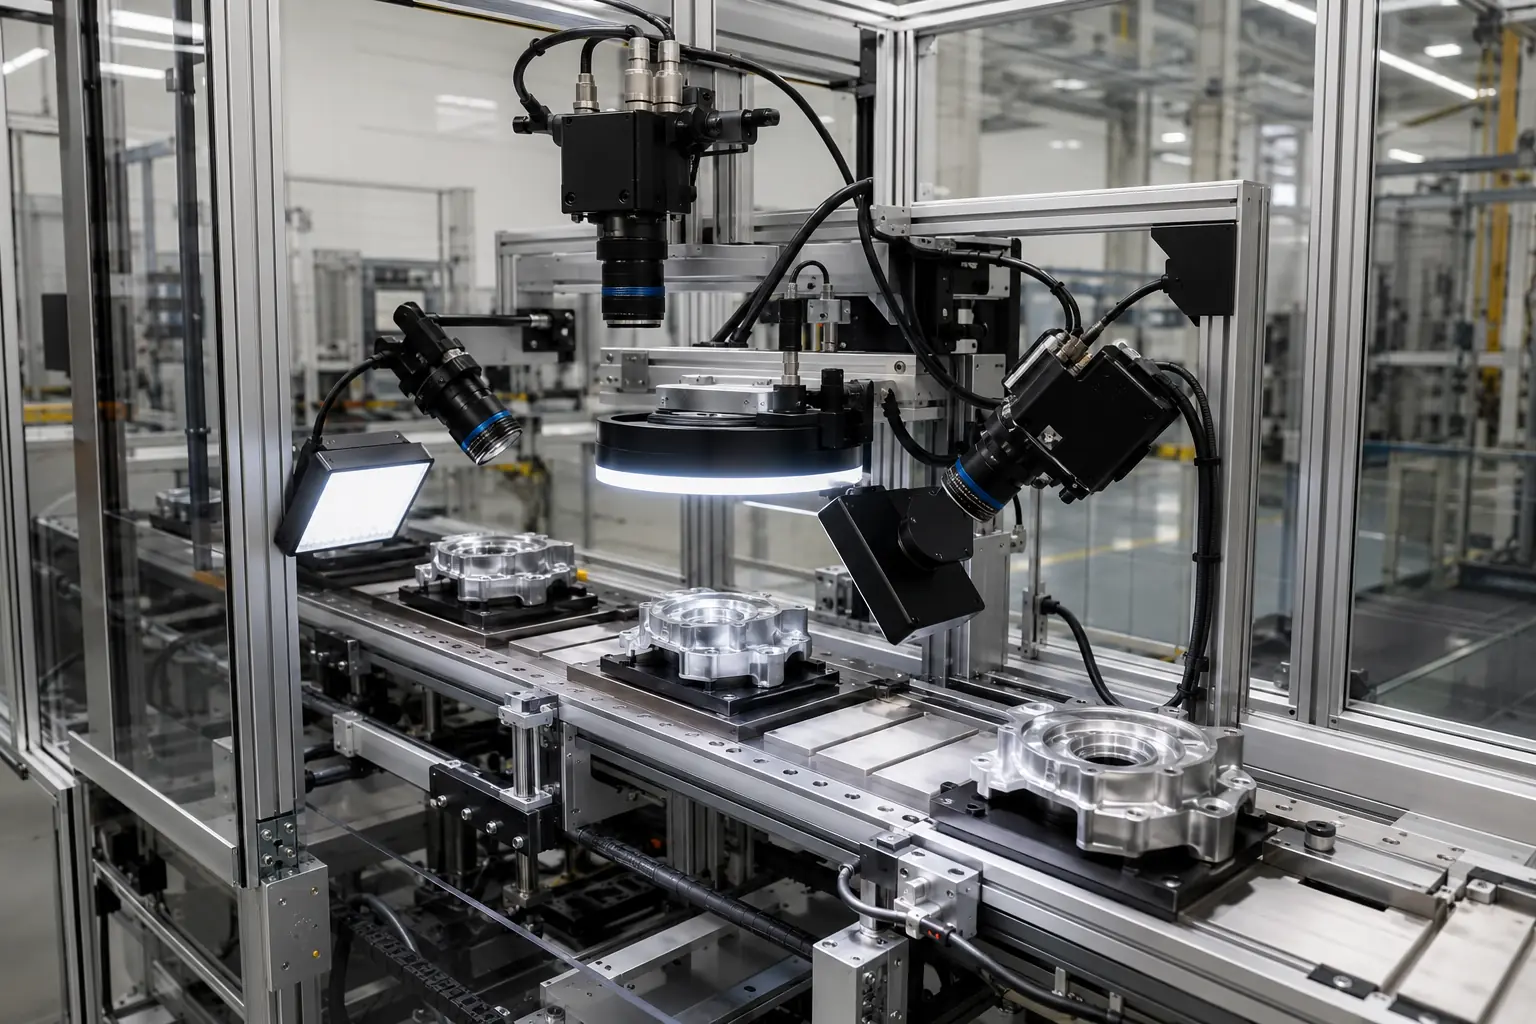 Complete system scope Optics, software, controls and mechanical integration.
Every item below is subject to application proof using the actual product, presentation and production conditions.
Configured against agreed examples, limits and the required line response.
Configured against agreed examples, limits and the required line response.
Configured against agreed examples, limits and the required line response.
Configured against agreed examples, limits and the required line response.
Configured against agreed examples, limits and the required line response.
Configured against agreed examples, limits and the required line response.
Detection is only useful when the result is delivered to the right control, operator or quality record at the right time.
Trigger a stable image using controlled lighting, suitable optics and repeatable product presentation.
Apply proven rules, measurements or trained models with product-specific acceptance limits.
Reject, divert, stop, alarm, guide automation or pass the result to production data systems.
No single optical set-up finds every possible defect. We define the defect set, size, contrast and viewing conditions, then test representative samples.
Often, yes, but reflections must be controlled using carefully positioned lighting, polarisation and sometimes multiple views.
AI can help where normal variation is complex, but conventional tools remain preferable when a deterministic rule solves the inspection reliably.
Send us samples, images, line-speed information and the defects you need to detect. We’ll recommend the right next step.