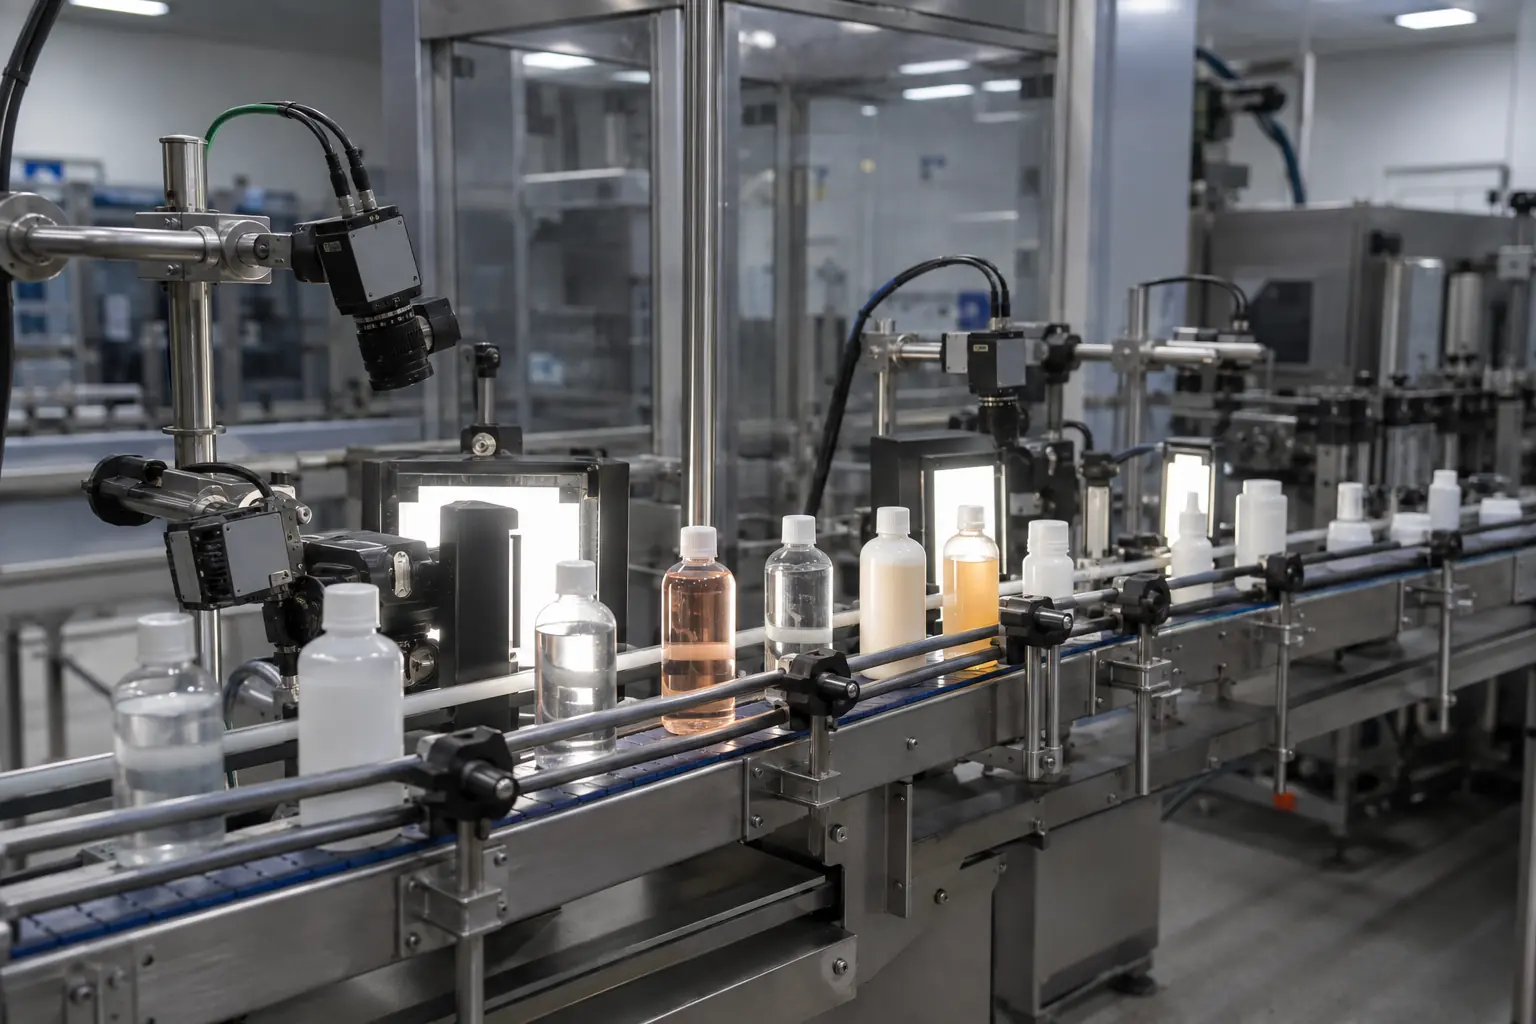
Cap, plug, seal and closure presence
Optics, lighting and acceptance logic configured for the product and line conditions.
Chemical production and packing lines require dependable checks on container, closure and identification. We specify suitable enclosures, materials and controls around the actual environment and product risk.
 Designed around the line Product, process, environment and response.
Chemical production and packing lines require dependable checks on container, closure and identification. We specify suitable enclosures, materials and controls around the actual environment and product risk.
We combine controlled imaging with production-ready mechanical and controls integration. The system can reject, divert, stop, alarm or pass data to a wider line architecture according to the agreed requirement.
How we prove an inspectionWe test the actual product, known defects and normal process variation before confirming the final method.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Ingress protection, materials, ventilation and any hazardous-area constraints must be established before equipment selection.
Rigid, flexible, opaque and translucent packs need different optical methods.
Vision can confirm presence and readable content, with the exact verification scope defined from samples and artwork.
A system may combine several checks and views into one product result.
Only when the complete application and area classification have been assessed and appropriately rated equipment is specified.
It can check label presence, identity, position and selected printed content where the optical conditions and artwork allow.
Standard visible-light vision cannot see through an opaque pack. Another measurement technology may be required.
Send us samples, images, line-speed information and the defects you need to detect. We’ll recommend the right next step.