Pack, tray and product presence
Optics, lighting and acceptance logic configured for the product and line conditions.
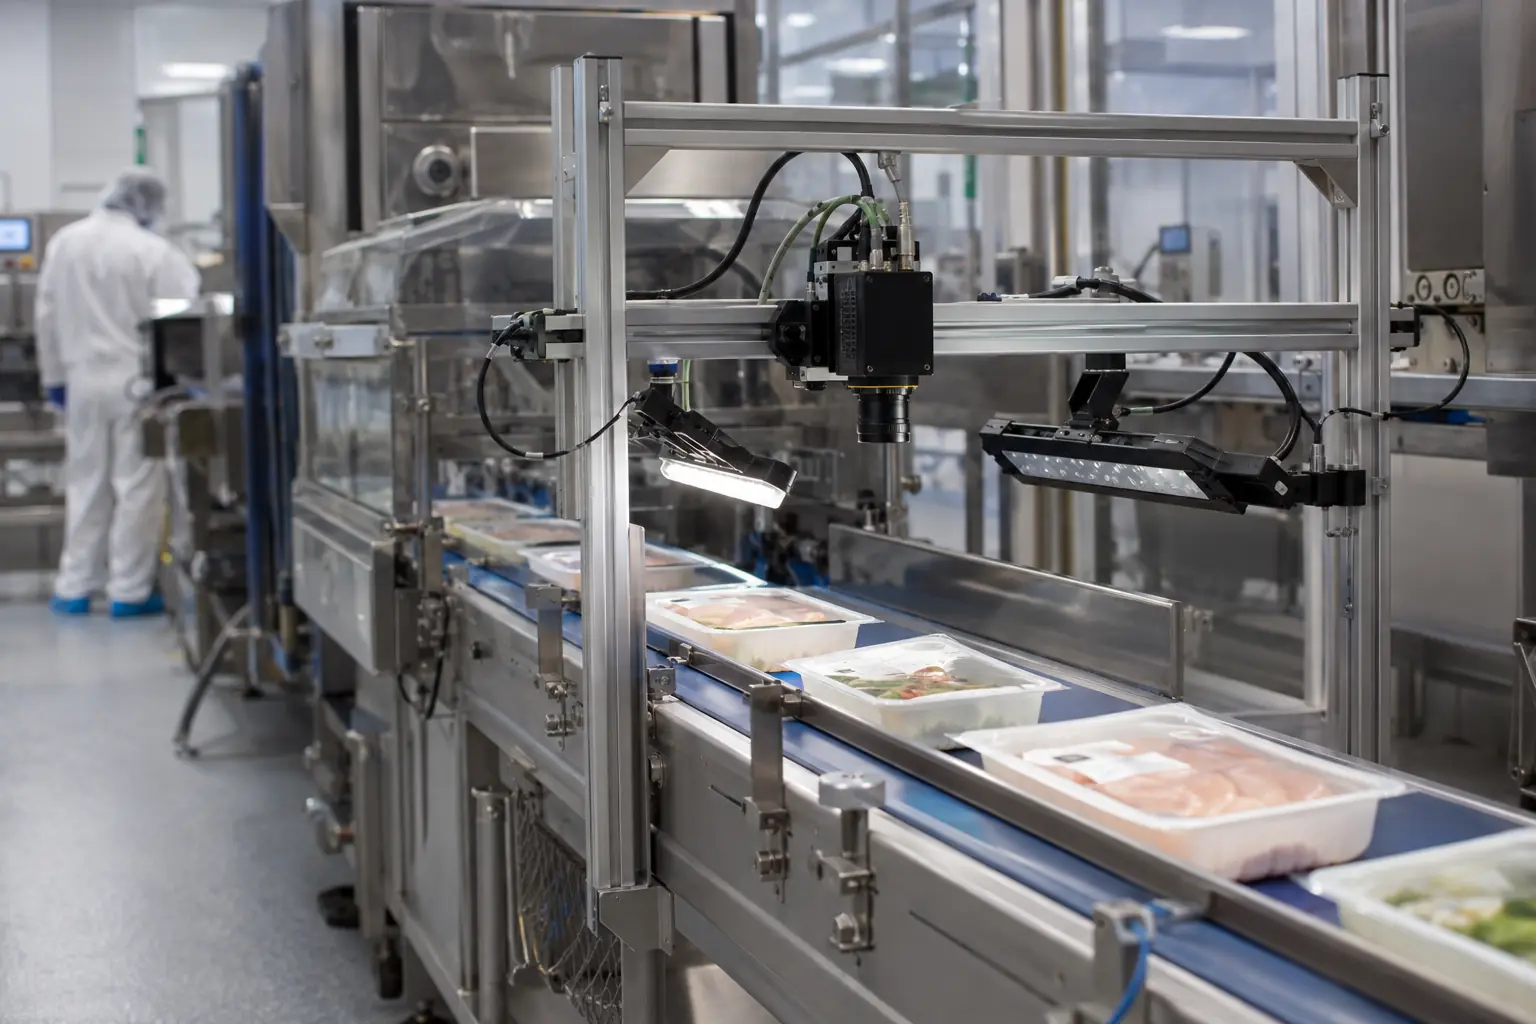
Food vision inspection systems provide repeatable checks without touching the product. We engineer hygienic camera and lighting arrangements around your pack format, product variation, washdown regime and line speed.
 Designed around the line Product, process, environment and response.
Food vision inspection systems provide repeatable checks without touching the product. We engineer hygienic camera and lighting arrangements around your pack format, product variation, washdown regime and line speed.
We combine controlled imaging with production-ready mechanical and controls integration. The system can reject, divert, stop, alarm or pass data to a wider line architecture according to the agreed requirement.
How we prove an inspectionWe test the actual product, known defects and normal process variation before confirming the final method.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Materials, enclosures, cable routing and mounting are selected around the production zone and cleaning method.
Acceptance limits are developed from representative good product as well as known defects.
Inspection, tracking and rejection are coordinated so the correct pack is removed without disrupting production.
A system may combine several checks and views into one product result.
Often, yes, although glare, film wrinkles and condensation must be assessed during sample testing.
It can, provided the acceptable range is represented during development and the optical conditions are controlled.
Presence, position and readable-code checks can be specified, subject to print quality, contrast and code format.
Send us samples, images, line-speed information and the defects you need to detect. We’ll recommend the right next step.