Cap, crown, cork and closure presence
Optics, lighting and acceptance logic configured for the product and line conditions.
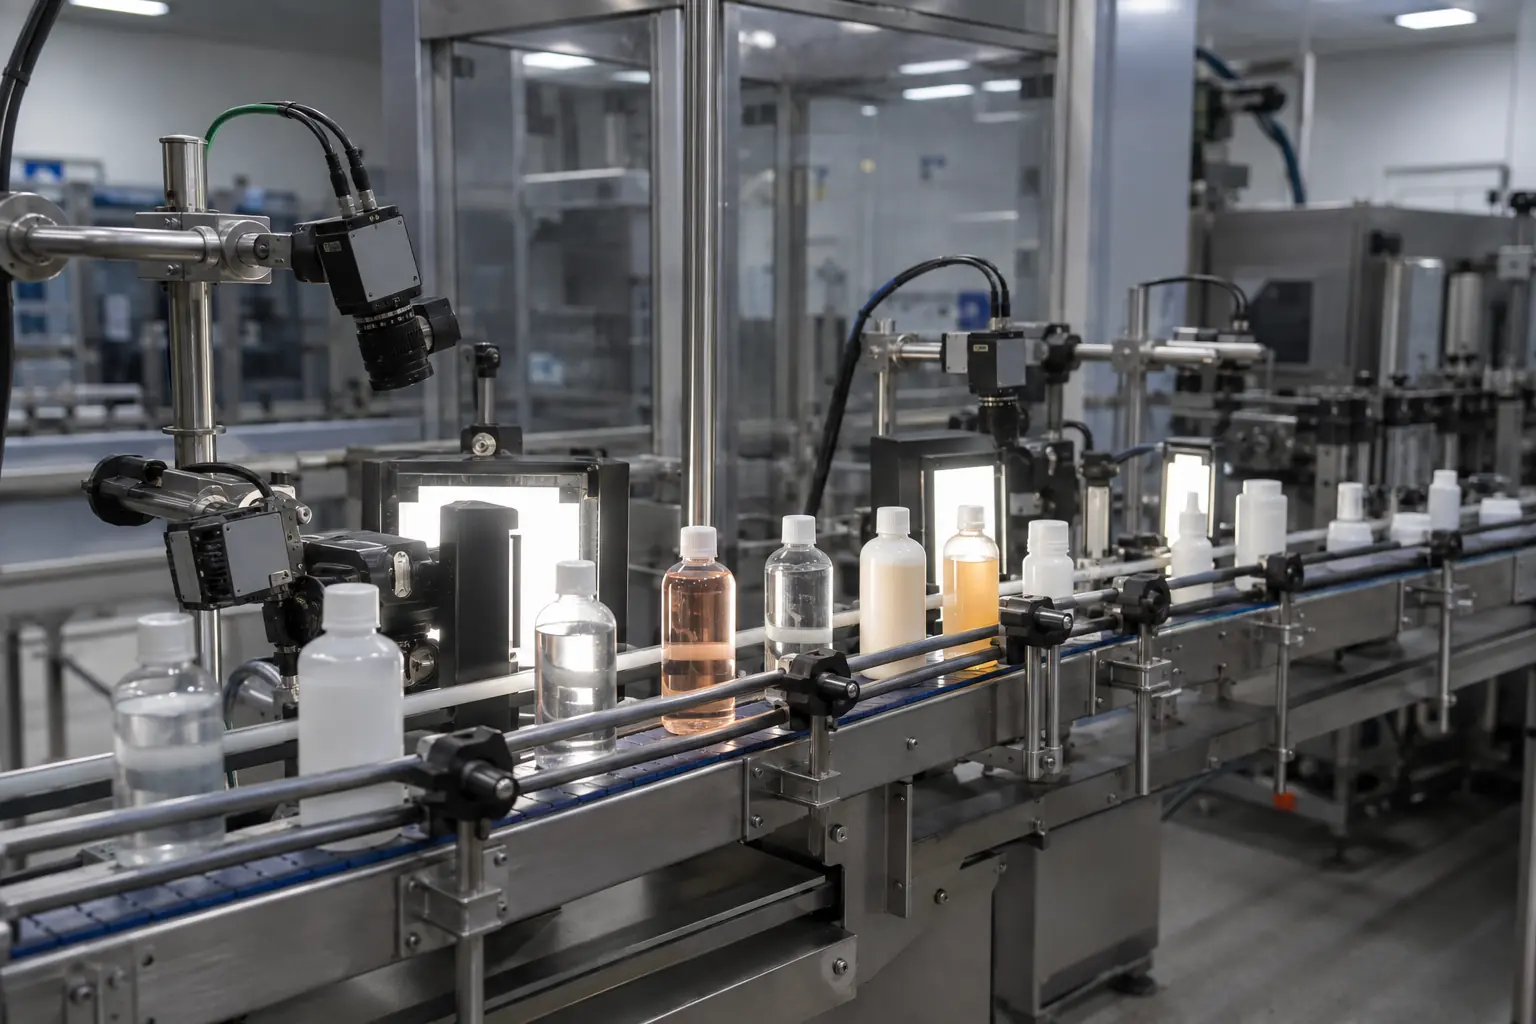
Beverage lines demand fast, reliable decisions on moving containers. We integrate cameras, lighting, tracking and reject control around the container, closure and pack presentation.
 Designed around the line Product, process, environment and response.
Beverage lines demand fast, reliable decisions on moving containers. We integrate cameras, lighting, tracking and reject control around the container, closure and pack presentation.
We combine controlled imaging with production-ready mechanical and controls integration. The system can reject, divert, stop, alarm or pass data to a wider line architecture according to the agreed requirement.
How we prove an inspectionWe test the actual product, known defects and normal process variation before confirming the final method.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Optics, lighting and acceptance logic configured for the product and line conditions.
Triggering, exposure and reject timing are engineered against real conveyor speed and container pitch.
Diffuse lighting, polarisation and carefully selected viewing angles help manage reflective containers.
Recipes can coordinate inspection limits, product tracking and operator changeover instructions.
A system may combine several checks and views into one product result.
Yes, for many checks. The achievable result depends on the container, liquid, label and background contrast.
Vision can check visible height, angle and feature position; torque itself requires a suitable mechanical measurement method.
Yes, when the conveyor, spacing, tracking and reject device are designed together for the required line rate.
Send us samples, images, line-speed information and the defects you need to detect. We’ll recommend the right next step.